


| Quantity: | |
|---|---|
| Product Overview |
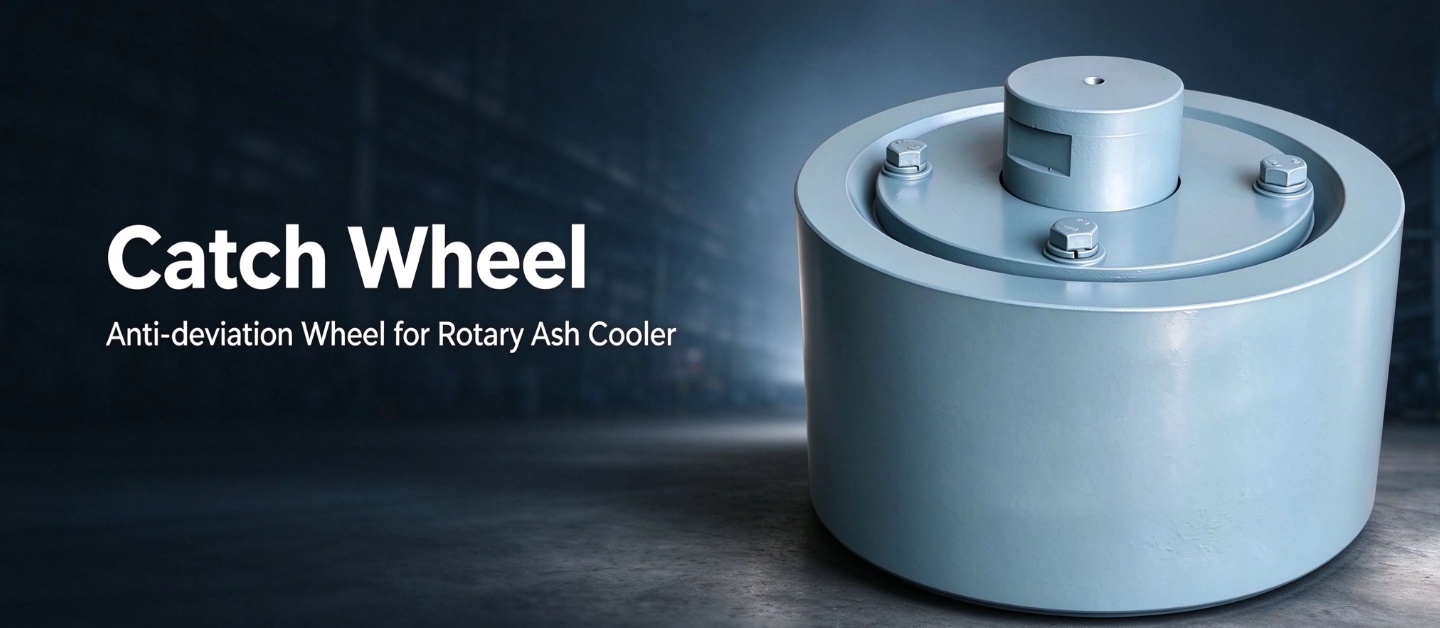
This Catch Wheel and Anti-deviation Wheel set is engineered for rotary ash coolers, where a Support Wheel carries radial load and a Support Ring limits axial travel. Supplied as a complete Support Wheel Assembly, the unit is cast in ZG270-500, machined with HB180-260 hardness control and finished in anti-rust paint. As a long-term Rotary Ash Cooler Spare Parts supplier we also build CFB Boiler Slag Cooler Parts to drawing, so the Rotary Ash Cooler Catch Wheel and Slag Cooler Anti-deviation Wheel you order fit the drum position first time. Every Painted Anti-deviation Wheel Assembly is inspected for concentricity, bolt spacing and keyway size before packing, and ships in fumigation-free cases with material certificates. Send your drawing and we quote within 24 hours, with 15-25 days production and 12 months warranty. |
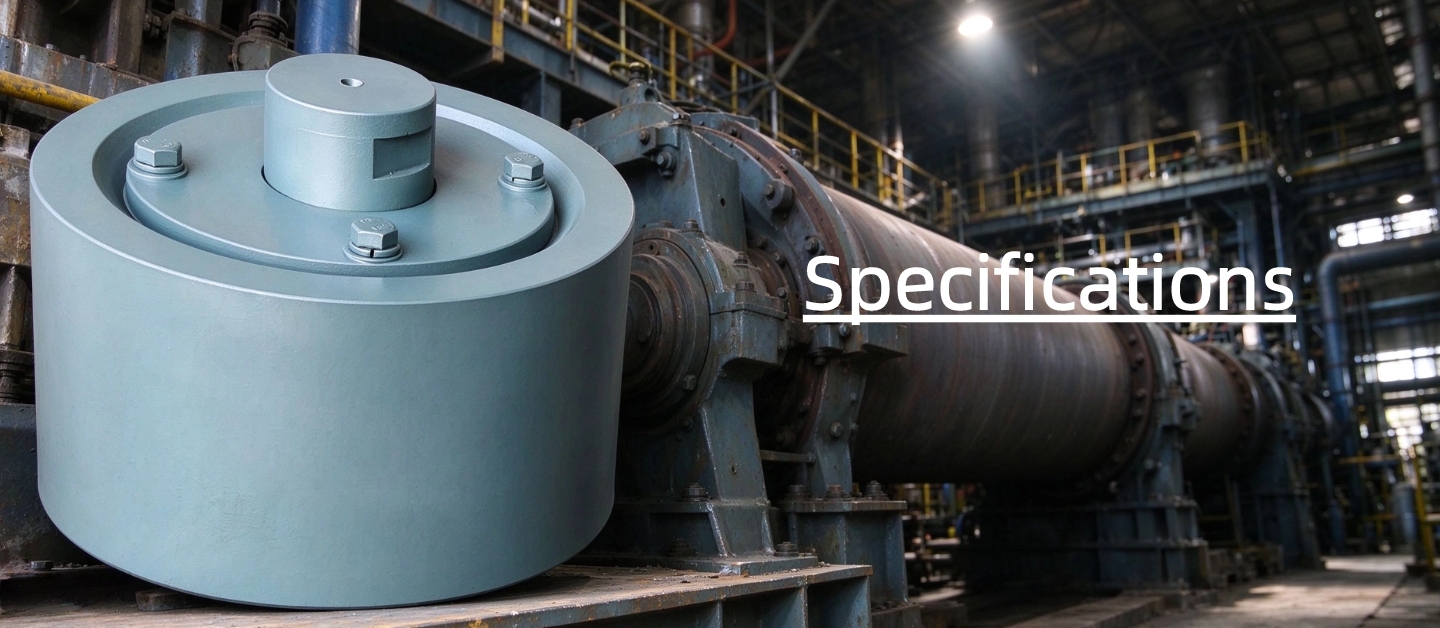
| 1 | Product Name | Catch Wheel / Anti-deviation Wheel |
| 2 | Alternative Names | Support Wheel, Thrust Wheel, Alignment Wheel |
| 3 | Application | Rotary Ash Cooler, CFB Boiler Slag Cooler |
| 4 | Material | ZG270-500 cast steel ZG270-500 |
| 5 | Hardness | HB180-260 |
| 6 | Working Temperature | Up to 300 degrees C |
| 7 | Supply Form | Machined blank / Painted assembly |
| 8 | Surface Treatment | Machined natural / Zinc-rich primer + topcoat |
| 9 | Standard Colour | Light blue-grey |
| 10 | Bolts | 4 hex socket screws (blank) / 3 hex bolts (assembly) |
| 11 | Keyway | Radial keyway on centre shaft |
| 12 | Mounting | Square base plate with two threaded holes |
| 13 | Dimensions | To be confirmed by drawing |
| 14 | Tolerance | Per drawing and agreed standard |
| 15 | Lubrication | Grease replenished every 3-6 months |
| 16 | Inspection | Hardness, concentricity, bolt spacing recorded |
| 17 | Documents | Material cert, hardness report, dimensional record |
| 18 | Packing | Fumigation-free plywood case |
| 19 | MOQ | Negotiable |
| 20 | Lead Time | 15-25 days standard, 25-35 days customized |
| 21 | Warranty | 12 months |
| 22 | Port | Qingdao, China |
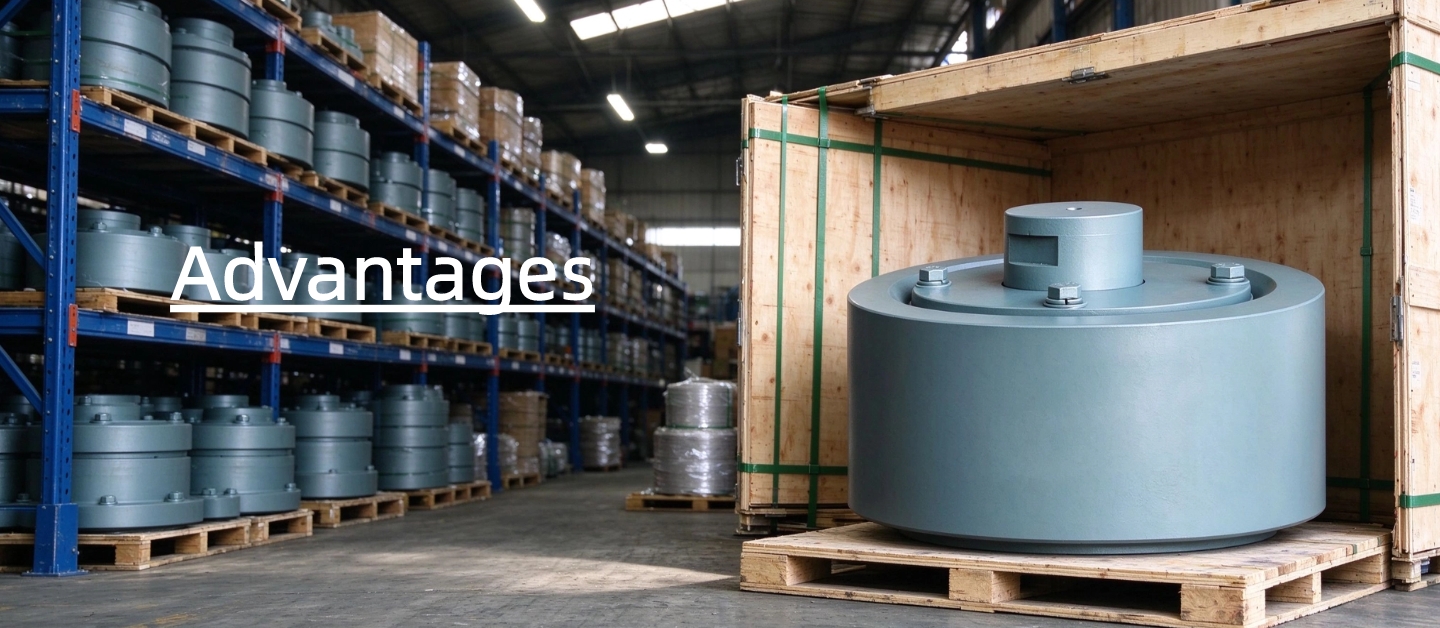
| 1 | Cast in ZG270-500 cast steel, the Catch Wheel body holds stable strength under the drum's axial thrust and keeps alignment through long continuous slag handling runs. |
| 2 | Hardness is controlled at HB180-260, a balance between wear resistance and machinability that suits the abrasive slag flow inside rotary ash coolers. |
| 3 | Both the machined blank and the painted assembly come from the same casting batch, so a customer can stock blanks and finish them locally without changing dimensions. |
| 4 | The Anti-deviation Wheel limits axial travel of the drum while the Support Wheel takes radial load, so the two parts share duty and neither bearing is overloaded. |
| 5 | A complete Support Wheel Assembly ships pre-matched with ring, bolts and keyway checked, cutting site assembly time and preventing mismatched spare parts on the shelf. |
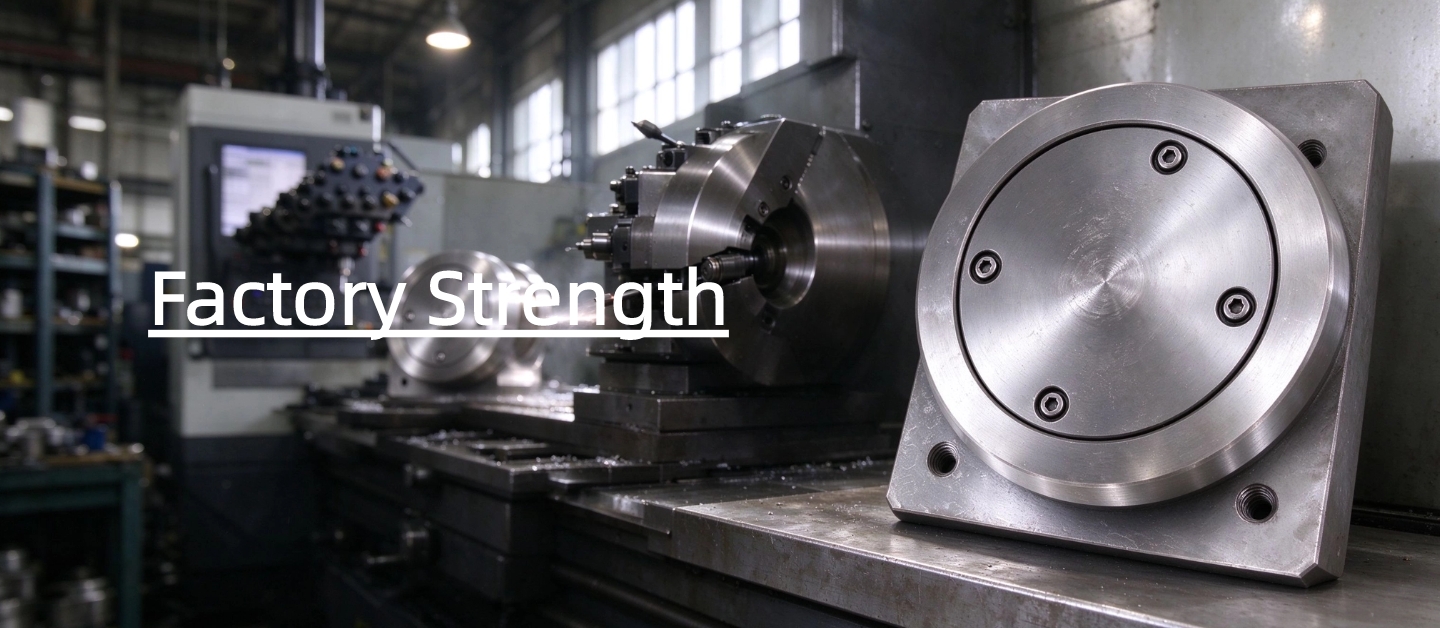
| 6 | Mounting faces are machined in one setup, keeping the base plate square to the wheel axis so the part seats flat on the frame without shimming. |
| 7 | Bolt holes and threaded mounting holes are drilled on CNC with template control, matching the original equipment footprint and allowing direct replacement. |
| 8 | The keyway on the centre shaft is cut to the drawing width and depth, so the coupling or drive key seats fully and avoids rocking under torque. |
| 9 | Concentricity of the wheel body to the mounting centre is measured on every batch, keeping the drum running true and reducing vibration at the support position. |
| 10 | Surface roughness on the contact face is machined to a fine finish, lowering friction against the drum end ring and extending the service interval. |
| 11 | The painted assembly uses zinc-rich primer plus topcoat, giving corrosion protection that survives humid plant air and occasional washdown. |
| 12 | Paint dry film thickness and gloss are recorded per batch, so the delivered colour stays consistent when you reorder months later. |
| 13 | Standard colour is a light blue-grey, and a colour number can be matched to your existing equipment so new parts do not stand out on site. |
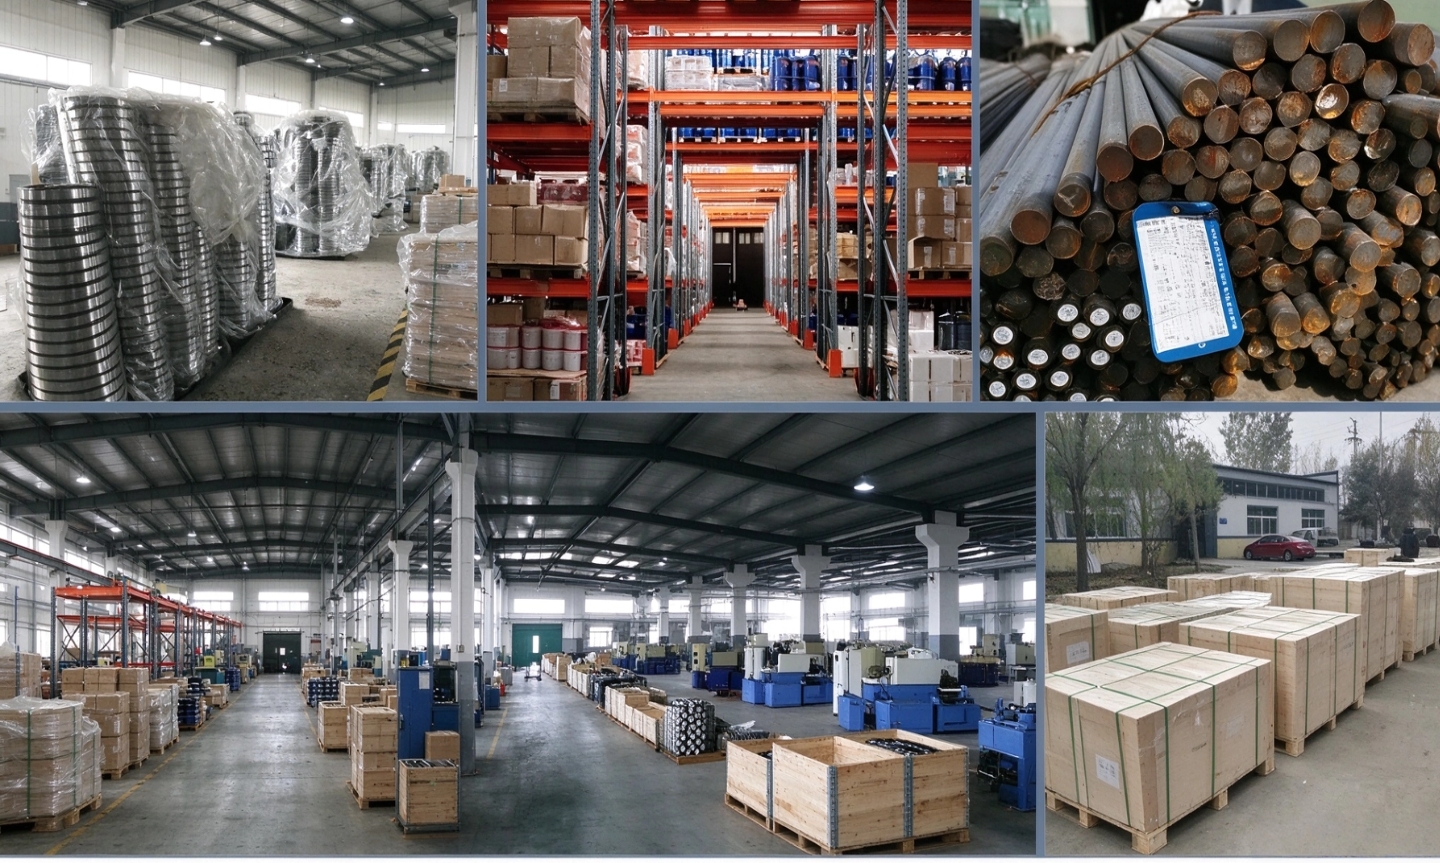
| 14 | Each unit is checked against the drawing for overall height, ring diameter and bolt spacing before packing, and the record travels with the goods. |
| 15 | Material certificates, hardness reports and dimensional records are issued as a document set, supporting ISO and customer audit requirements. |
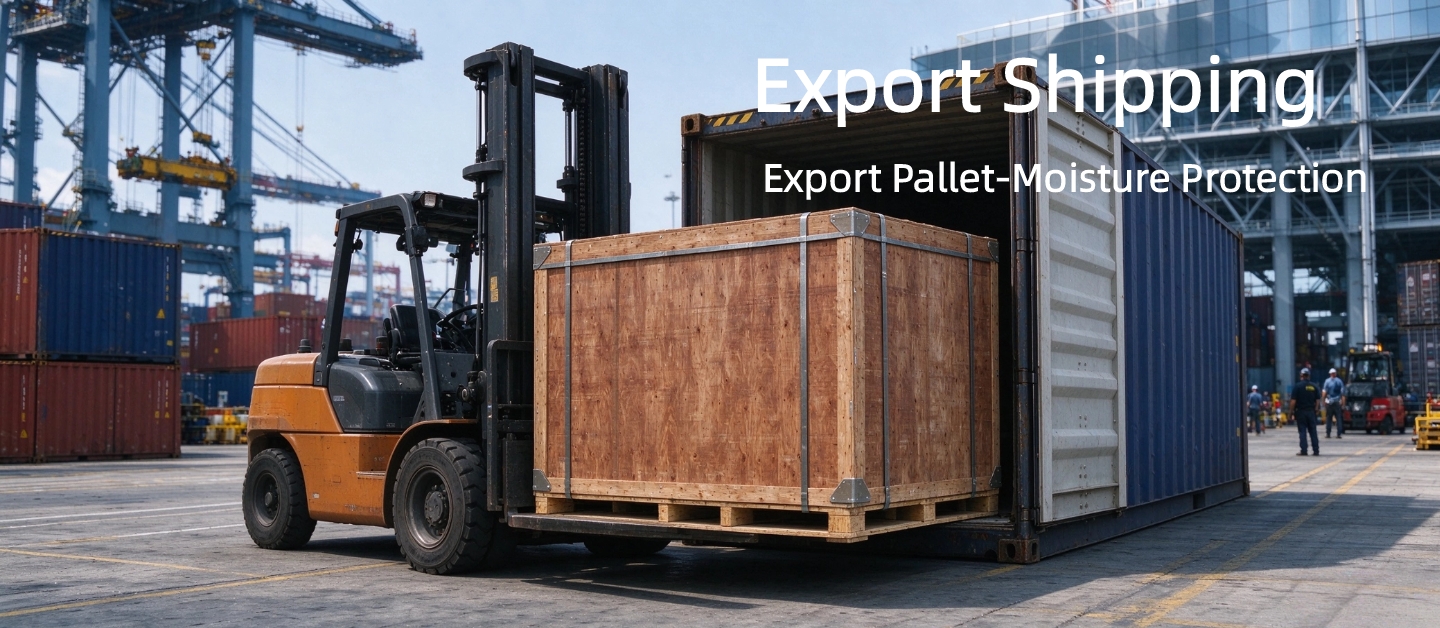
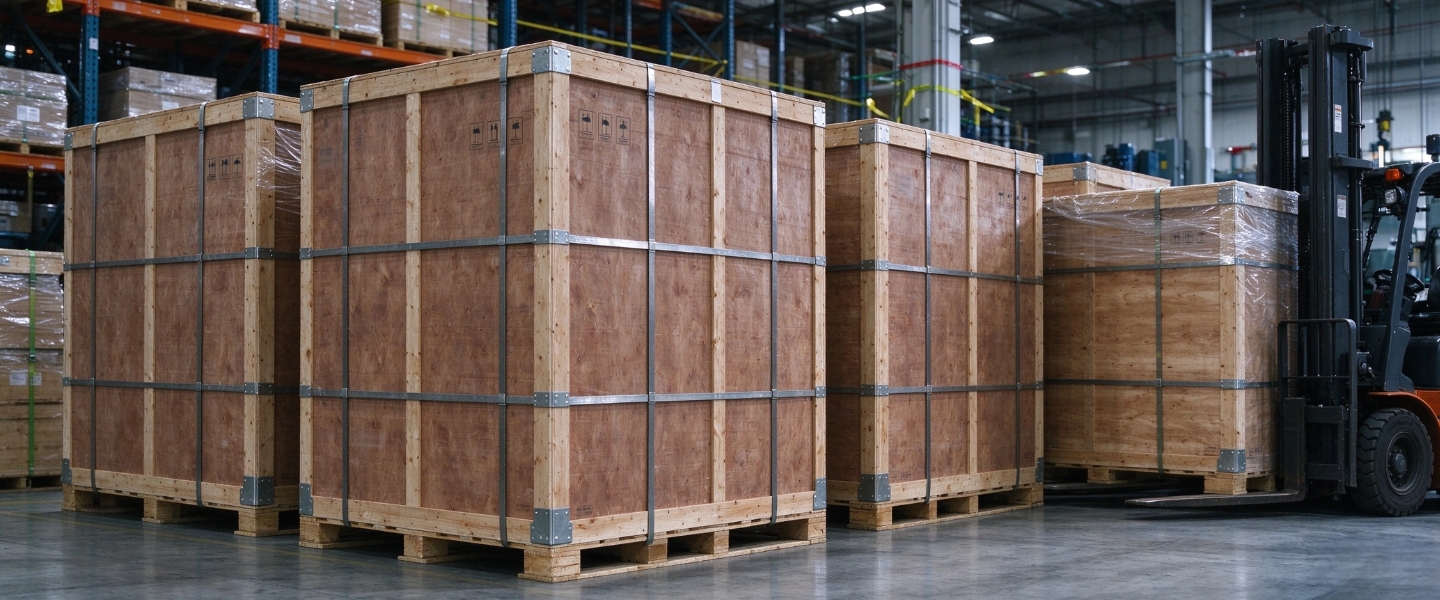
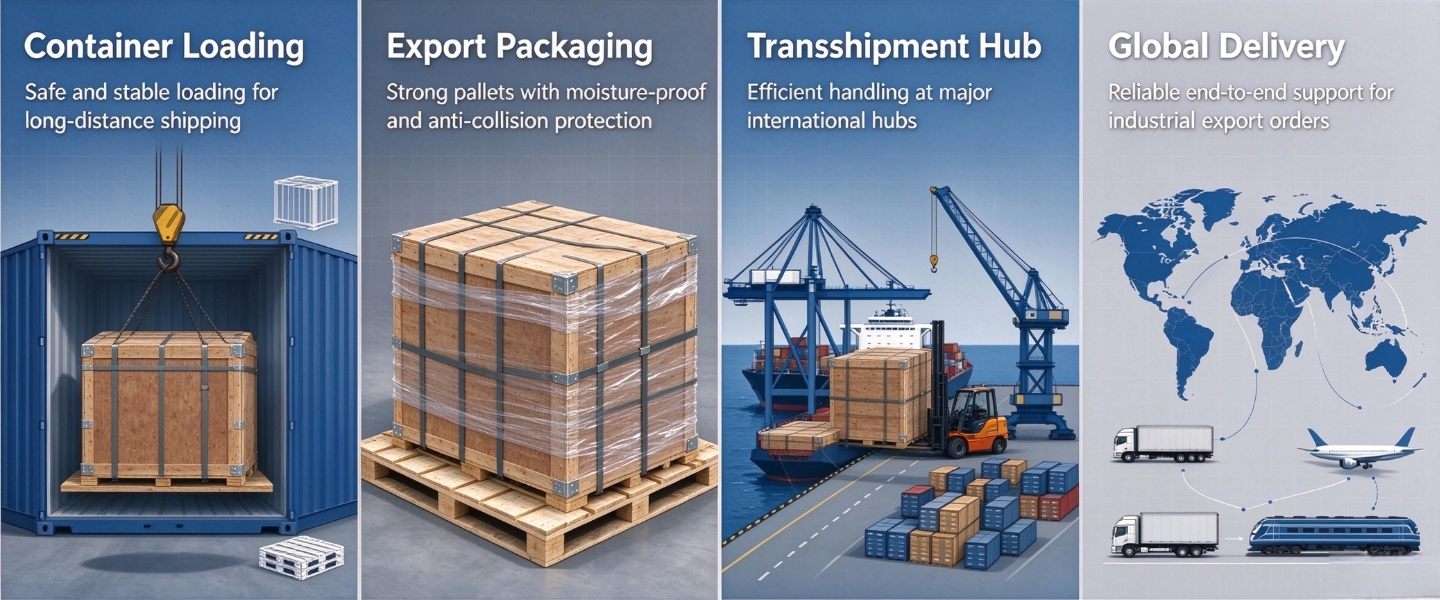
| 16 | Fumigation-free plywood cases with rust preventive film and desiccant keep the machined faces dry through long ocean transit. |
| 17 | Modules are blocked and braced inside the case, and heavy units are lifted by marked points, reducing transit damage and unloading risk. |
| 18 | Mixed loading is supported: catch wheels, support rings, thrust wheels and bolts can share one container to cut freight per spare part. |
| 19 | Standard production runs 15 to 25 days after drawing confirmation, and customized castings take 25 to 35 days, fitting planned boiler overhaul windows. |
| 20 | Samples or first articles can be supplied before batch production, so the maintenance team can trial fit the part on the drum before committing to volume. |
| 21 | The same drawing version is kept on file, so repeat orders in the following years are machined to the original dimensions without re-discussion. |
| 22 | Both supply forms are available in one order: painted assemblies ready to bolt on plus machined blanks for local finishing and stocking. |
| 23 | Because the part is a wearing alignment component, keeping one spare on the shelf avoids a full production stop when the drum starts drifting. |
| 24 | The design suits rotary ash coolers from different boiler makers; matching is done by mounting drawing rather than by brand name. |
| 25 | Applications cover thermal power, biomass, metallurgy and chemical plants, including CFB boiler slag handling systems and lime or gypsum powder coolers. |
| 26 | Working temperature up to 300 degrees C is acceptable with standard grease, and higher temperature duty can be met by changing the lubricant grade. |
| 27 | Grease is replenished every 3 to 6 months depending on load, keeping a simple maintenance routine without special tools. |
| 28 | A 12 month warranty covers casting defects and machining errors, and replacement parts are shipped from stock for urgent shutdown cases. |
| 29 | Technical support includes mounting photos, tightening sequence and clearance guidance, helping fitters install correctly the first time. |
| 30 | As a factory supplier we quote from drawing within 24 hours, keep MOQ negotiable and ship worldwide from Qingdao port with export documents handled in house. |
FAQ
| 1 | Does the Catch Wheel replace the Support Wheel? | No. The Support Wheel carries radial load, while the Catch Wheel limits axial movement. Both are needed on a rotary ash cooler. |
| 2 | Which part actually stops the drum from drifting? | The Anti-deviation Wheel acts on the drum end face and stops axial drift; the Support Ring provides the contact face it works against. |
| 3 | Can you supply only the machined blank? | Yes. The Machined Catch Wheel Blank ships before painting so you can finish it with your own coating system. |
| 4 | Is the painted assembly ready to install on arrival? | Yes. It is coated with primer and topcoat; only bolting and clearance check are needed on site. |
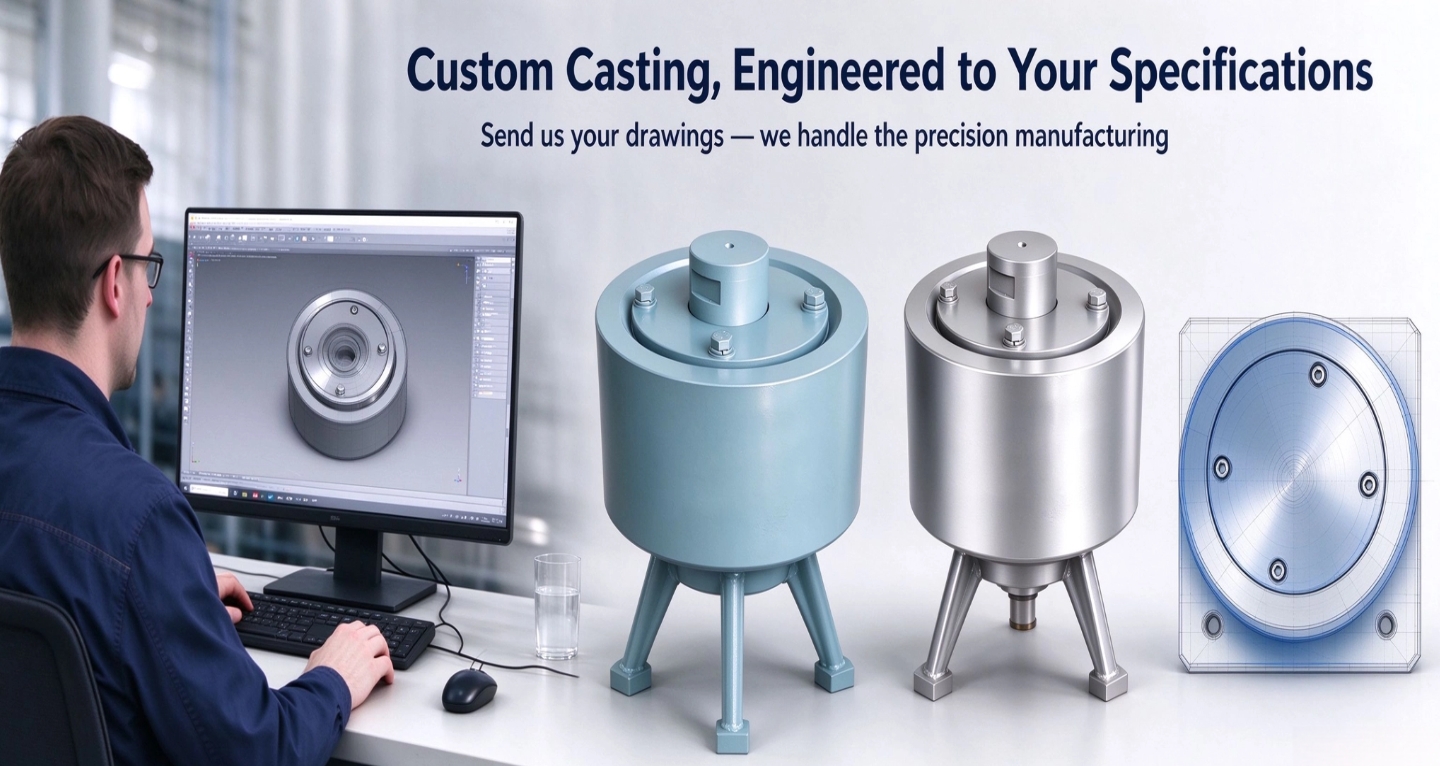
| 5 | Can dimensions be customized? | Yes. Send a 2D drawing or 3D model and we machine to your centre height, bolt spacing and keyway size. |
| 6 | How is hardness controlled? | Body hardness is held at HB180-260 and tested per batch, with the report issued with the goods. |
| 7 | What is the maximum working temperature? | Up to 300 degrees C with standard grease; higher temperature duty needs a changed lubricant grade. |
| 8 | Do you provide material certificates? | Yes. Material certificate, hardness report and dimensional record are issued as a document set. |
| 9 | What is the MOQ? | MOQ is negotiable; trial orders of a few pieces are accepted for first cooperation. |
| 10 | How long is production? | 15 to 25 days after drawing confirmation, and 25 to 35 days for customized castings. |
| 11 | Can I get a sample before ordering? | Yes, a sample or first article can be supplied for trial fit before batch production. |
| 12 | How are the parts packed for sea freight? | Fumigation-free plywood cases with rust preventive film, desiccant and blocking inside. |
| 13 | Can several spare parts share one container? | Yes. Catch wheels, support rings, thrust wheels and bolts can be mixed in one shipment. |
| 14 | Do you handle export documents? | Yes. Invoice, packing list, certificate of origin and other required papers are prepared in house. |
| 15 | What warranty applies? | 12 months covering casting defects and machining errors, with spare parts available from stock. |
| 16 | Which industries use this part? | Thermal power, biomass, metallurgy and chemical plants running rotary ash coolers or powder coolers. |
| 17 | Does it fit coolers from other makers? | Matching is by mounting drawing, not by brand, so most rotary ash coolers can be served. |
| 18 | Why does the drum drift in the first place? | Uneven load, worn support rings or misaligned frames cause drift; the catch wheel resets the limit but the cause should be checked too. |
| 19 | How often should grease be added? | Every 3 to 6 months depending on load and temperature, using the grade specified in the manual. |
| 20 | Can the colour match our equipment? | Yes. A colour number or sample can be matched; standard is light blue-grey. |
| 21 | Do you supply the matching support ring? | Yes. Support Ring and bolts can be supplied as a set with the catch wheel. |
| 22 | What surface finish is used on the contact face? | The contact face is machined to a fine finish to reduce friction against the drum end ring. |
| 23 | Is there a tightening sequence for the bolts? | Yes, tighten in a diagonal sequence to the torque given in the drawing, and recheck after the first run. |
| 24 | What if the keyway does not fit? | Send photos and dimensions; we check against the archived drawing and supply a corrected part. |
| 25 | Can you produce from our 3D model? | Yes. 2D drawing or 3D model both work; we confirm the first article before batch production. |
| 26 | How do I verify incoming quality? | Check hardness with a portable tester, measure bolt spacing and concentricity, and compare with the documents supplied. |
| 27 | Is the part repairable? | Light scoring on the contact face can be re-machined; cracked castings should be replaced rather than welded. |
| 28 | What causes abnormal noise after replacement? | Usually clearance or alignment; recheck mounting face flatness and drum end ring wear. |
| 29 | Can you hold stock for our annual overhaul? | Yes, a stock agreement can be set with a reserved quantity shipped on call. |
| 30 | Do you support OEM branding? | Yes. Private label cartons, nameplates and shipping marks can be arranged. |
| 31 | How do I start an order? | Send the drawing, quantity and destination port; we reply with quotation, lead time and packing plan within 24 hours. |


